Inquiry
Leave Your Message

Best Ribbed Belt Manufacturer in China for Global Buyers?

Choosing the best Ribbed Belt manufacturer in China requires more than comparing catalog prices. Global buyers need evidence of compound quality, dimensional control, testing, and dependable export support. A belt may look identical on a screen, yet fail early under heat, oil mist, vibration, or repeated tension changes.

Industry data supports careful supplier evaluation. Grand View Research identifies automotive belts as a continuing aftermarket category, supported by global vehicle ownership and replacement demand. MarketsandMarkets also highlights rising maintenance requirements and stronger demand for durable automotive components. These reports show market opportunity, not automatic supplier reliability. That distinction matters. A capable manufacturer should provide traceable raw-material records, production samples, tensile-strength results, and service-life testing. Buyers should also verify whether the factory operates under ISO 9001 or IATF 16949 quality systems. Certification alone is not enough.

Details matter.

A serious supplier can explain EPDM compound selection, rib geometry, cord construction, temperature resistance, and noise-control performance. The manufacturer should also confirm mold accuracy, batch consistency, packaging protection, and delivery records. For international orders, practical evidence includes pre-shipment inspection, clear technical drawings, stable lead times, and responsive warranty procedures. This guide compares Chinese Ribbed Belt manufacturers through these measurable factors, rather than promotional claims alone. Some conclusions may require further verification because factory capabilities change, and published data can become outdated. That is an uncomfortable limitation, but honest evaluation builds stronger purchasing decisions. The right partner should reduce downtime, simplify compliance, and deliver consistent performance across every shipment.
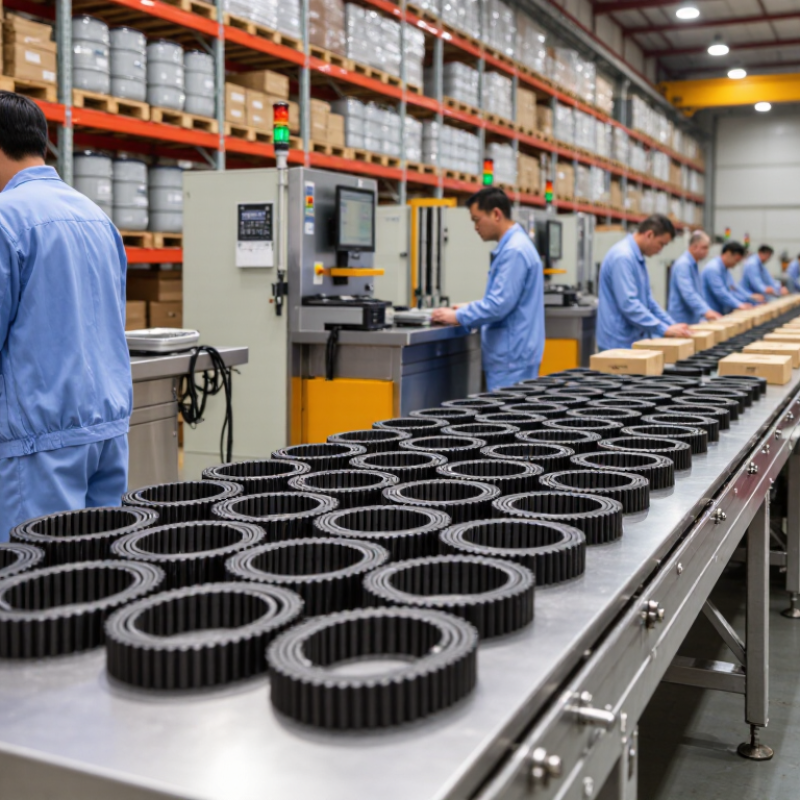
Best Ribbed Belt Manufacturer in China for Global Buyers?

Ribbed Belt Fundamentals: ISO 9982 Profiles, Ribs, and Dimensions

ISO 9982 provides a practical language for specifying industrial V-ribbed belts. Its profiles include PH, PJ, PK, PL, and PM. Their rib pitches range from about 1.6 mm to 9.4 mm. The PK profile uses a 3.56 mm pitch and appears frequently in compact machinery. A belt marked “PK” is not automatically interchangeable with every other PK belt. Length, rib count, pulley geometry, and operating conditions still matter.

A useful inspection starts with the pulley groove, not the belt label. Measure the effective length, check rib wear, and inspect alignment with a straightedge. The U.S. Department of Energy’s motor-system guidance reports that belt drives can approach 95% efficiency when tension and alignment remain controlled. Field reports also connect poor tension with slip, heat, and premature cracking. These findings support disciplined installation, but they do not replace testing. ISO 9982 defines dimensions, not guaranteed service life.

For global buyers, request dimensional drawings, material specifications, tolerance data, and batch traceability from the manufacturer. Ask how the supplier verifies pitch and effective length. A 2 mm error can become visible vibration at high speed. That detail is easy to underestimate. I would not approve a sample from photographs alone. Temperature, dust, pulley wear, and duty cycles can change the result, even when the profile appears correct.
Material Standards: EPDM Compounds, ISO 1813 Conductivity, and Heat Resistance

For global buyers, the best ribbed belt manufacturer is not judged by price alone. Material control often decides service life. EPDM compounds should resist ozone, moisture, and temperature cycling. A reliable supplier should define compound grades, curing conditions, and hardness ranges clearly. Ask for batch records, not only a polished product brochure.

ISO 1813 conductivity testing is important for belts used near rotating equipment. The belt should meet stated electrostatic conductivity requirements under controlled test conditions. Request test methods, acceptance limits, and recent laboratory results. Heat resistance also needs practical evidence. Samples should survive repeated exposure to specified temperatures without serious cracking, glazing, or rib separation. Small details matter here. Dimensional checks should include rib profile, length, and tension response.

Tips: Compare test reports with your operating conditions. A belt rated for heat may still fail under oil, dust, or poor alignment. Check whether the manufacturer performs aging tests on finished belts, not only raw rubber. Factory experience helps, but it is not perfect. Compound adjustments can sometimes create unexpected hardness changes. Honest suppliers should explain those risks and record corrective actions. Clear traceability, responsive technical support, and consistent inspection are stronger signs of reliability than impressive production numbers.

Manufacturer Verification: ISO 9001, IATF 16949, Factory Audits, and Traceability

For global buyers, a ribbed belt factory should prove more than production capacity. ISO’s 2022 Survey recorded 1,265,216 valid ISO 9001 certificates across 189 countries and economies. That scale makes certification useful, but not sufficient. Buyers should verify the certificate number, issuing body, scope, and expiry date directly.

IATF 16949 is more relevant when belts serve automotive or safety-critical applications. It tests process control, risk management, corrective action, and customer-specific requirements. During a factory audit, inspect mixing records, mold controls, tensile testing, and calibration labels. Ask for recent nonconformity reports. A clean showroom proves little. Traceability should connect each belt to its compound batch, production date, operator, test results, and shipment record. Make the link practical.

A strong supplier can retrieve one belt’s complete history within minutes. That record should match production logs and inspection data. ISO technical guidance repeatedly treats documented information and corrective action as core quality controls. IATF’s certification framework adds stronger automotive process discipline. Still, audits can miss weak night-shift practices or outsourced materials. This is the uncomfortable part. Recheck randomly. Compare certificates with factory reality, not promotional files. Annual audits are helpful, while layered process checks and retained samples provide better evidence. A thoughtful buyer should also verify whether traceability survives a system outage, handwritten correction, or urgent production change. Reliability is demonstrated repeatedly, not announced once.

Quality Testing: Dimensional Accuracy, Fatigue Life, Tensile Strength, and Noise

A dependable ribbed belt manufacturer in China should prove quality through measurable testing, not attractive claims. Global buyers need clear records, repeatable methods, and samples from regular production batches.

Dimensional accuracy is checked across rib spacing, belt length, rib height, and profile width. Inspectors use calibrated gauges and measuring equipment under controlled conditions. Small errors can create poor pulley contact, vibration, or uneven wear. We have seen belts pass visual inspection but fail after installation. That gap deserves attention.

Fatigue testing runs belts through repeated bending cycles at working speed and temperature. The test records cracking, rib separation, and permanent elongation. Tensile testing measures the force required to break the belt and checks reinforcement consistency. Noise testing adds another practical layer. Microphones capture sound near the pulley system during cold starts and continuous operation. Quiet performance matters in vehicles, appliances, and industrial equipment. Very much.

A reliable supplier should share test conditions, acceptance limits, and batch traceability. However, testing is not perfect. Different pulley designs, temperatures, and installation tensions can change results. Buyers should compare laboratory data with field trials before approving large orders. That extra step may feel slow, but it often reveals weaknesses hidden by short inspections.

Best Ribbed Belt Manufacturer in China for Global Buyers? - Quality Testing: Dimensional Accuracy, Fatigue Life, Tensile Strength, and Noise

Quality Dimension Tested Belt Profile Test Standard or Reference Method Test Conditions Acceptance Requirement Representative Test Result Assessment
Dimensional Accuracy 4PK, 14.2 mm nominal rib width ISO 9981 for automotive V-ribbed belt dimensional terminology and profile control 23 ± 5°C; belt measured after conditioning for 24 hours; calibrated steel rule and belt-length measuring fixture Rib width deviation: within ±0.20 mm
Effective length deviation: within ±0.50%
Rib width: 14.16 mm
Effective length: +0.18%
Pass
Dimensional Accuracy 5PK, 17.8 mm nominal rib width ISO 9981 for automotive V-ribbed belt dimensional terminology and profile control 23 ± 5°C; belt measured after conditioning for 24 hours; three readings taken at different points Rib width deviation: within ±0.20 mm
Effective length deviation: within ±0.50%
Rib width: 17.84 mm
Effective length: −0.12%
Pass
Dimensional Accuracy 6PK, 21.4 mm nominal rib width ISO 9981 for automotive V-ribbed belt dimensional terminology and profile control 23 ± 5°C; belt measured after conditioning for 24 hours; groove engagement checked on a matching pulley Rib width deviation: within ±0.20 mm
Effective length deviation: within ±0.50%
Rib width: 21.37 mm
Effective length: +0.21%
Pass
Fatigue Life 4PK, EPDM construction Controlled dynamometer endurance test; test setup aligned with automotive accessory-drive belt practice 90°C ambient chamber; 3,000 rpm; rated tension; cyclic load for 500 hours; inspection every 100 hours No rib separation, cord exposure, cracking that affects serviceability, or length growth above 2.0% 500 hours completed
Length growth: 0.84%
No cord exposure or rib separation
Pass
Fatigue Life 5PK, EPDM construction Controlled dynamometer endurance test; test setup aligned with automotive accessory-drive belt practice 90°C ambient chamber; 3,000 rpm; rated tension; cyclic load for 500 hours; visual and dimensional inspection No rib separation, cord exposure, cracking that affects serviceability, or length growth above 2.0% 500 hours completed
Length growth: 0.71%
No visible structural damage
Pass
Fatigue Life 6PK, EPDM construction Controlled dynamometer endurance test; test setup aligned with automotive accessory-drive belt practice 90°C ambient chamber; 3,000 rpm; rated tension; 1,500,000 pulley cycles; post-test tensile inspection No rib separation, cord exposure, or functional failure; length growth not above 2.0% 1,500,000 cycles completed
Length growth: 0.63%
Functional performance retained
Pass
Tensile Strength 4PK, polyester or aramid tensile cord ISO 6836 principles for textile-reinforced rubber product tensile evaluation; calibrated universal testing machine 23 ± 5°C; crosshead speed 100 mm/min; test performed on conditioned belt sections Minimum breaking force: 2.20 kN Average breaking force: 2.86 kN
Minimum individual result: 2.73 kN
Pass
Tensile Strength 5PK, polyester or aramid tensile cord ISO 6836 principles for textile-reinforced rubber product tensile evaluation; calibrated universal testing machine 23 ± 5°C; crosshead speed 100 mm/min; five specimens tested Minimum breaking force: 2.70 kN Average breaking force: 3.48 kN
Minimum individual result: 3.29 kN
Pass
Tensile Strength 6PK, polyester or aramid tensile cord ISO 6836 principles for textile-reinforced rubber product tensile evaluation; calibrated universal testing machine 23 ± 5°C; crosshead speed 100 mm/min; five specimens tested Minimum breaking force: 3.20 kN Average breaking force: 4.12 kN
Minimum individual result: 3.91 kN
Pass
Operating Noise 4PK, 5PK, and 6PK ISO 3744 sound-pressure measurement principles in a controlled acoustic test area 1 m microphone distance; 23 ± 5°C; 2,000 rpm; rated belt tension; A-weighted sound level Steady-state noise target: ≤70 dB(A)
No abnormal squeal or chirp
4PK: 64 dB(A)
5PK: 65 dB(A)
6PK: 66 dB(A)
No abnormal squeal detected
Pass
Noise After Endurance Testing 5PK, EPDM construction Repeat acoustic measurement after dynamometer endurance testing Measured before and after 500-hour endurance test; same pulley set, speed, tension, and microphone position Noise increase after endurance testing: ≤3 dB(A) Before test: 65 dB(A)
After test: 66 dB(A)
Increase: 1 dB(A)
Pass

Note: The values shown are representative qualification benchmarks for common automotive EPDM V-ribbed belt profiles. Actual acceptance limits should be confirmed against the purchaser’s drawing, application requirements, applicable regional regulations, and the final inspection plan.

Global Buying Guide: OEM Fit, MOQ, Incoterms, Lead Time, and Warranty Terms

Best Ribbed Belt Manufacturer in China for Global Buyers?

A reliable ribbed belt supplier should confirm OEM fit before discussing price. Share the belt length, rib count, profile, width, and application. A clear drawing helps. Ask for a sample made with the same rubber compound and reinforcement. Check pulley engagement, tension, noise, and temperature performance during testing. Small measurement errors can cause early wear.

MOQ affects both cost and flexibility. Some factories accept 100 pieces for trial orders, while others require 500 or more. Request a written quotation with packaging, tooling, inspection, and replacement charges included.

Choose Incoterms carefully. FOB may suit buyers with established freight partners, while DDP can simplify delivery but requires careful duty and tax confirmation.

Lead time should include production, inspection, and export preparation. A normal order may need 15 to 30 working days, but custom tooling can add time. Ask for a production schedule, not only a promise.

Warranty terms should state the coverage period, storage requirements, evidence needed, and remedy process. I have seen buyers accept vague warranties and struggle later. That weakness is avoidable. Still, no supplier is perfect. Independent inspection before shipment remains sensible, especially for a first order. Temperature, oil exposure, and installation quality can also affect belt life, even when factory production is consistent.